EN

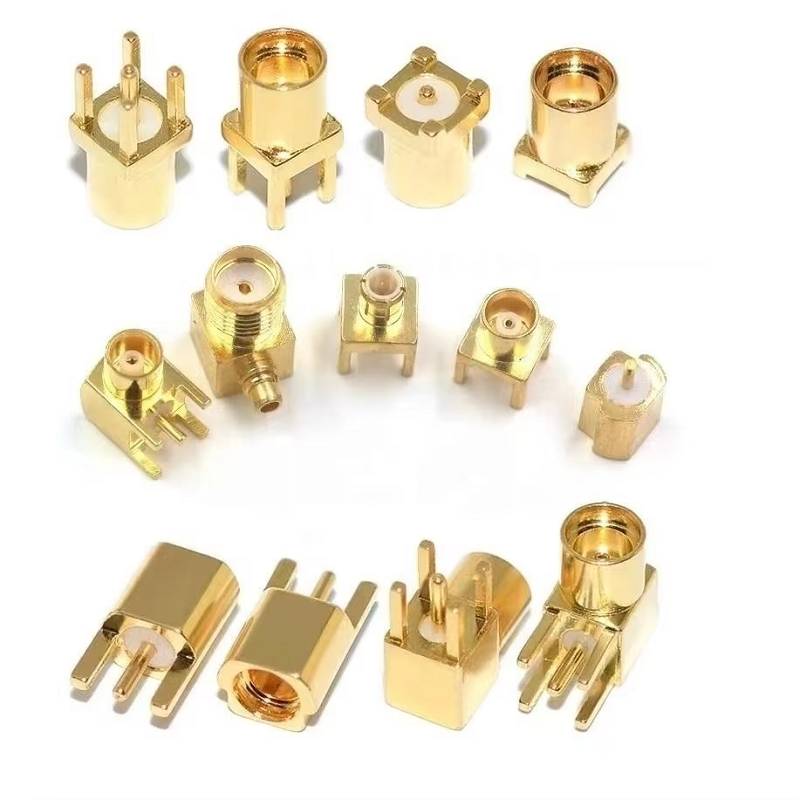
In modern high-density RF engineering, circuit board real estate is at a premium. When conventional subminiature interfaces like SMA or SMB prove too bulky for ultra-compact enclosures, a micro-miniature solution becomes essential for maintaining reliable high-frequency signal transmission. The mmcx connector fills this critical hardware gap, providing a compact 50 Ohm interconnect for space-constrained wireless equipment without sacrificing overall signal integrity or shielding performance.
Selecting the right micro-miniature rf coaxial connector requires evaluating the entire signal path rather than treating the mating face as an isolated mechanical detail. Operating frequency limits, maximum power handling capacity, mechanical retention forces, dielectric materials, and cable exit angles must align perfectly with overall system requirements to guarantee long-term operational stability.
Mechanical Architecture of Micro-Miniature RF Interfaces
The mmcx interface is a micro-miniature rf coaxial connector standardized under international specifications like IEC 61169-52. Engineered as a scaled-down relative of the older MCX series, it delivers a substantial footprint reduction that allows microwave design engineers to pack multiple parallel RF channels onto dense printed circuit boards.
| Feature | MMCX Specifications | MCX Comparison | SMA Comparison |
| Coupling Mechanism | Snap-on (360-degree rotation) | Snap-on | Threaded (1/4-36 UNS) |
| Footprint Size | Micro-miniature | Miniature | Standard Subminiature |
| Standard Impedance | 50 Ohm | 50 Ohm / 75 Ohm | 50 Ohm |
| Typical Frequency Range | DC to 6 GHz | DC to 6 GHz | DC to 18 GHz |
| Primary Deployment | Internal RF leads & IoT modules | Compact equipment & GPS | Test benches & microwave gear |
Unlike threaded connector options that require dedicated wrench clearance for installation, the snap-on coupling mechanism permits full 360-degree rotation after mating. This rotatable feature prevents torsional stress on delicate coaxial cables during final equipment assembly and field service. However, because the center contact pin, outer spring shield, and internal PTFE dielectric are scaled down significantly, mechanical tolerances during manufacturing directly dictate insertion loss, return loss, and physical contact reliability over repeated mating cycles.
Deployment Scenarios across Wireless Systems
Compact micro-miniature RF interfaces are widely deployed across modern industries where weight, vertical height, and overall board area are tightly controlled.
-
Internal Antenna Connections: Linking internal patch antennas and flexible PCB radiators to cellular modems, Wi-Fi 6 access points, and multi-constellation GNSS receivers.
-
Portable Test Instruments: Providing lightweight interconnects inside handheld spectrum analyzers, signal generators, and field diagnostic gear.
-
Medical Electronics: Enabling low-profile signal routing inside wearable telemetry monitoring pads and mobile diagnostic imaging hardware.
-
Unmanned Systems: Serving as vibration-tolerant antenna feeds inside commercial drones, robotic platforms, and compact IoT telemetry hubs.
-
Automotive Telematics: Connecting compact vehicle tracking devices, emergency call systems, and wireless infotainment modules inside crowded dashboard assemblies.
When choosing an mmcx interface for production builds, engineers must evaluate whether the connection is mated once during factory assembly or repeatedly serviced during field maintenance. For environments exposed to heavy mechanical vibration, constant thermal cycling, or accidental cable pulling, adding molded strain relief boots or securing the cable with mechanical chassis clips prevents premature engagement failure and contact wear.
Evaluating Right-Angle Connector Transitions
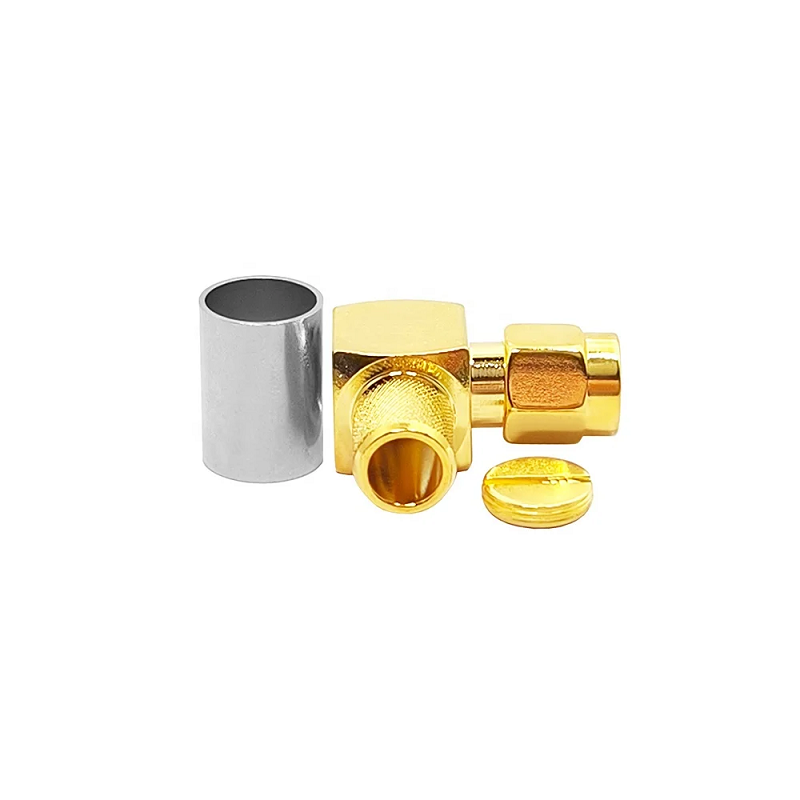
In tight enclosure designs where vertical clearance is extremely restricted, straight connectors can force flexible coaxial cables beyond their recommended minimum bend radius. This tight bending places dangerous side loads on surface-mount PCB jacks, risking solder joint fatigue or board trace delamination. Integrating a 90 degree coaxial cable connector solves spatial constraints by keeping cable runs completely parallel to the circuit board surface.
However, an engineered right-angle transition is not simply a straight connector bent at 90 degrees. The internal corner geometry alters the internal electrical field, creating potential impedance discontinuities if the internal transmission line is not precisely compensated.
-
Mechanical Clearance: Verify rear-panel depth, enclosure lid tolerances, and neighboring component height before specifying right-angle connector housings.
-
Bend Radius Protection: Ensure the cable exit angle prevents dielectric crushing and braid shield deformation at the connector ferrule junction.
-
Electrical Verification: Demand Vector Network Analyzer sweep data showing Voltage Standing Wave Ratio and insertion loss across the entire intended operating band, rather than relying solely on basic DC continuity checks.
-
Thermal Expansion: Account for mechanical expansion and contraction of internal dielectrics when operating across wide temperature ranges in outdoor RF enclosures.
Impedance Matching and Return Loss Control
Maintaining a clean 50 Ohm transmission path requires matching the connector impedance to the cable and board layout. Small physical variations in center pin diameter or outer conductor mating gaps create internal reflections, measured as high Voltage Standing Wave Ratio or poor return loss.
In high-frequency systems operating up to 6 GHz, impedance mismatches cause signal attenuation, phase distortion, and unwanted RF leakage. When selecting an rf coaxial connector, review published S-parameter data across the target frequency band. For critical signal paths, incorporating ground-coplanar waveguide circuit board launches ensures smooth transitions from the connector surface-mount pads to internal board traces.
System Selection Parameters for RF Design Engineers
To avoid unexpected signal dropouts and costly assembly line rework, follow a systematic evaluation framework when specifying high-density coaxial components:
-
Signal Budget: Confirm system impedance, operating bandwidth, and maximum allowable return loss. Treat generic DC to 6 GHz product claims as a theoretical ceiling that requires empirical validation for your specific application.
-
Power and Thermal Limits: Evaluate continuous wave power capacity at maximum operating ambient temperatures, factoring in frequency-dependent dielectric heating and current limits.
-
Cable Compatibility: Match connector ferrule dimensions precisely to miniature coaxial lines such as RG178, RG196, RG316, or ultra-thin micro-coaxial cable families.
-
Environmental Exposure: Determine if additional moisture sealing, corrosion-resistant body plating, or mechanical shielding is required for outdoor cabinets or harsh industrial environments.
-
Quality Verification: Require supplier lot inspection records, including center-contact plating thickness checks, dimensional verification, and high-frequency return loss sweep reports.
Field Assembly and Cable Termination Best Practices
Achieving repeatable performance with micro-miniature connectors requires strict adherence to assembly procedures and specialized tooling.
-
Precision Cable Stripping: Use calibrated strip tools to cut outer jackets, shield braid, and dielectric layers to exact manufacturer dimensions. Damaging the center conductor strands introduces micro-fractures that degrade high-frequency performance.
-
Controlled Center Contact Soldering: When soldering center contacts, apply controlled thermal energy to create a clean joint without melting surrounding PTFE dielectric material or causing solder wicking.
-
Uniform Shield Crimping: Ensure the outer shield braid is distributed evenly around the connector tail before crimping the ferrule with hex die tools calibrated to the specified crimp diameter.
-
Final Visual and Electrical Testing: Perform 100 percent continuity checks and visual inspection for center pin depth alignment, followed by sample sweep testing on network analyzers for high-reliability lots.
Manufacturing Precision and Supply Chain Quality
Reliable micro-miniature RF performance relies on strict manufacturing process controls, raw material purity, accurate cable stripping, and precise crimping techniques. Poor center-contact soldering or uneven outer braid crimping introduces immediate impedance reflections, compromises electromagnetic shielding, and degrades overall link budgets in critical wireless networks.
When project specifications demand verifiable high-frequency performance and complete lot traceability, partnering with experienced RF component manufacturers makes all the difference. Engineering teams around the globe depend on specialized suppliers like WORLDPEAK for precision-machined mmcx connectors, custom high-frequency cable assemblies, and specialized 90 degree coaxial cable connector solutions built to rigorous international standards.
By balancing electrical ratings, mechanical enclosure constraints, cable routing geometry, and robust supplier quality control, RF design engineers can confidently deploy compact interconnects that deliver long-term reliability and exceptional signal performance across demanding wireless applications.