EN

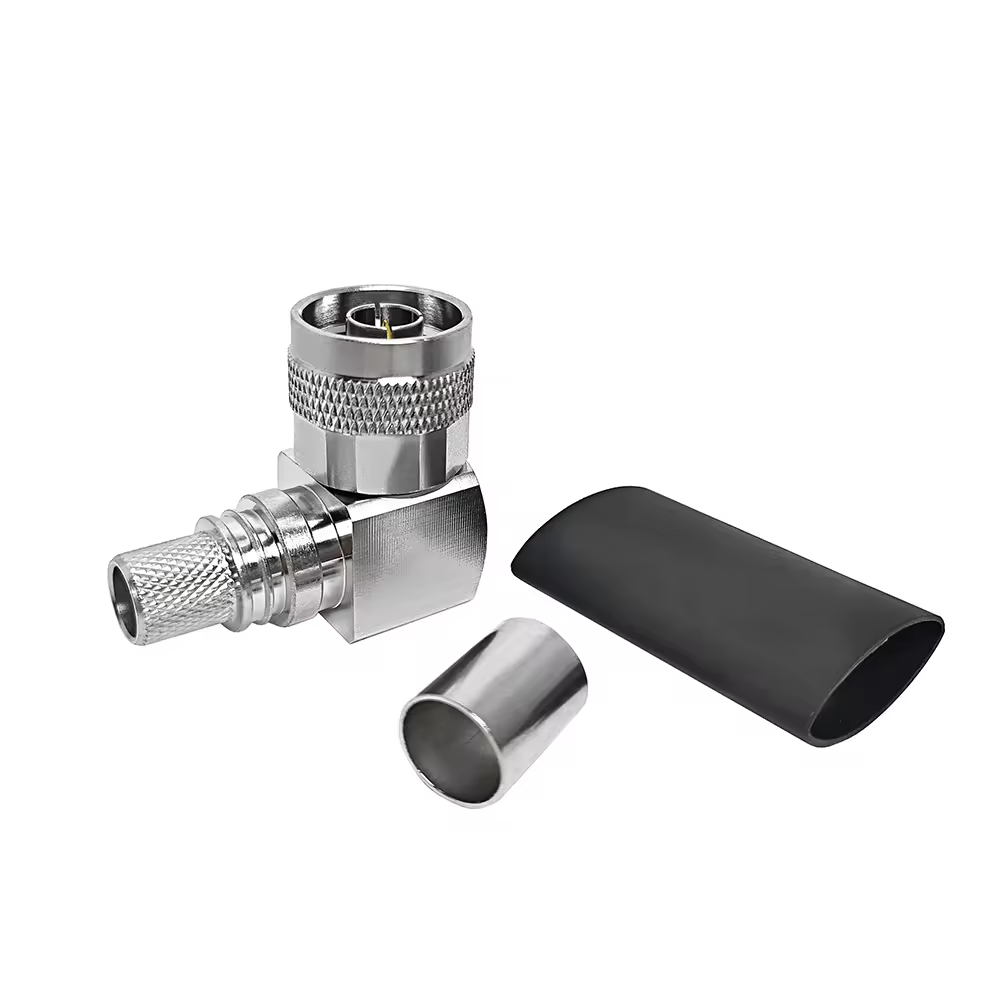
When an ODM engineering project calls for a 90 degree coax connector, solving physical clearance constraints is only half the design equation. The adapter functions as a critical junction along a high-frequency transmission line. Its impedance behavior must be calculated, measured, and locked into controlled drawings long before mass production tooling is approved.
Right-angle body geometries solve tight cabinet routing issues, yet they can easily introduce localized impedance discontinuities if the internal chamfer, dielectric geometry, pin transition, and test plan are handled as separate decisions.
For an RF development engineer, the primary question is never simply "Is this adapter 50 ohm or 75 ohm?" in isolation. The core engineering objective is identifying what impedance the complete path must maintain across its intended bandwidth, and establishing how the production team will prove it.
Building a clear confirmation sequence for a 90 degree coax connector ensures that prototype bench successes translate directly into repeatable factory releases.
Establishing System Impedance Before Cutting Metal
System designers must state nominal impedance requirements in the initial engineering brief. Most wireless, cellular, and microwave paths operate around a nominal 50 Ω baseline, whereas video broadcast, CATV, and specific instrumentation lines run on a 75 Ω standard.
Matching impedance comes from the system architecture rather than the physical angle of the housing. A 90 degree coax connector must match the internal dielectric profile of the mating family rather than just fitting external coupling threads.
Project teams should explicitly document mating interfaces, cable types, operating frequency ranges, signal levels, and reference cables used for laboratory validation.
A female to female coax cable connector might appear mechanically identical across catalog pages, yet electrical acceptance criteria differ significantly when frequency limits, power handling, or interface series change.
Converting Design Intent into Measurable Test Metrics
A usable ODM specification separates general design intent from hard pass-fail limits. Production drawings should include the following parameters:
-
Target System Impedance: State nominal values (50 Ω or 75 Ω) alongside interface standards like SMA, N-Type, or BNC.
-
Operating Frequency Band: Specify start and stop test frequencies (e.g., DC to 6 GHz) rather than using vague terms like "high frequency."
-
Reflection Criteria: Define acceptable limits using Voltage Standing Wave Ratio (VSWR) or Return Loss (dB) across the evaluated band.
-
Insertion Loss Thresholds: Establish maximum attenuation limits over the full operating frequency span.
-
Calibration Reference Planes: Document exact connector interfaces and calibration standards used during verification.
-
Quality Verification Rules: State sample sizes for prototype sign-off and specify whether production shipments require retained sweep plots.
VSWR serves as an effective metric because it quantifies reflected power magnitude in a clear format. Reflection limits must align directly with overall link budgets and system performance margins.
Evaluating Internal Geometry Before Tooling Release
The center conductor radius, dielectric support sleeve, outer cavity housing, and 90-degree turn geometry together determine how smoothly a 90 degree coax connector guides electromagnetic fields.
Engineering reviews should analyze cross-sectional internal views rather than focusing solely on external dimensions. Subtle variations in center-pin steps or dielectric support gaps alter local capacitance and inductance, causing impedance spikes at higher frequencies.
Internal geometric features directly impact local impedance:
-
Center Pin Corner Chamfer: Precision radiused pins help mitigate local capacitive spikes at the bend.
-
Dielectric Air Gaps: Tightly tolerated PTFE steps eliminate localized inductive discontinuities.
-
Outer Cavity Turn Radius: Compensated internal chamfers prevent severe field distortion and energy loss.
Reviewing practical interface factors early prevents downstream production delays:
-
Is the adapter configured as a bulkhead mount, PCB launch, or inline cable unit?
-
Will connected cabling exert bending torque on the body after final installation?
-
Does nearby enclosure metal interfere with coupling nuts or affect high-frequency fields?
Addressing these points is vital when a female to female coax cable connector is mounted inside a compact enclosure where connected cables apply uneven mechanical loads.
Constructing the VNA Test Plan Around Actual Use Cases
Vector Network Analyzer (VNA) sweep data provides concrete proof of electrical performance. Before sweeping samples, test engineers must document calibration methods (such as SOLT), calibration planes, coupling torque settings, test port adapters, sweep point density, and frequency bounds.
Using clean, undamaged test ports is essential; worn calibration adapters can introduce artificial reflections that mimic part defects.
-
Calibrate the VNA for chosen test ports and interface types using documented standards.
-
Inspect interface mating faces, align pins carefully, and apply recommended coupling torque.
-
Sweep the designated band to capture S11 return loss and S21 insertion loss traces.
-
Perform remating tests to verify mechanical repeatability across multiple connection cycles.
-
Compare measured reflection traces directly against approved drawing limits rather than generic catalog sheets.
When evaluating a 90 degree coax connector, sweep the entire functional assembly—including mating connectors, housing transitions, and representative cable runs. Omitting key transitions during bench tests risks missing real-world reflections.
Using Reflection Traces for Root-Cause Analysis
VNA sweep traces function as diagnostic tools for refining prototype geometry. A narrow reflection peak indicates a localized geometric discontinuity inside the adapter body, whereas a broad upward trend across the band points to mismatched dielectrics, poor cable terminations, or calibration errors.
Engineers should verify calibration validity, mating alignment, and fixture integrity before altering production drawings. When adjusting internal dimensions, retaining earlier trace logs alongside drawing revisions allows teams to confirm that geometry tweaks genuinely improved higher-frequency performance.
This disciplined approach avoids confusion when sourcing teams reference a female to female coax cable connector. The title describes gender configuration, but it does not define impedance tolerances, frequency capabilities, or required VNA test methods.
Establishing Controlled Releases for High-Volume Production
Prototype approval should produce a frozen engineering record. The final release package should contain approved drawing revisions, nominal impedance definitions, operational frequency bounds, calibration specs, sample sweep plots, and signed first-article inspection (FAI) reports.
Moving from prototype validation to volume manufacturing requires a reliable interconnect supplier. WORLDPEAK provides specialized RF connector and adapter engineering, custom OEM/ODM development, and comprehensive pre-shipment electrical testing—including 100% VSWR and insertion-loss sweep inspection.
By defining exact system impedance goals, interface series, and VNA test criteria from the start, WORLDPEAK helps engineering teams transform 90 degree coax connector designs into reliable, high-performance production components.