EN
How Suppliers Implement Strict Quality Control on OEM N Type Connector
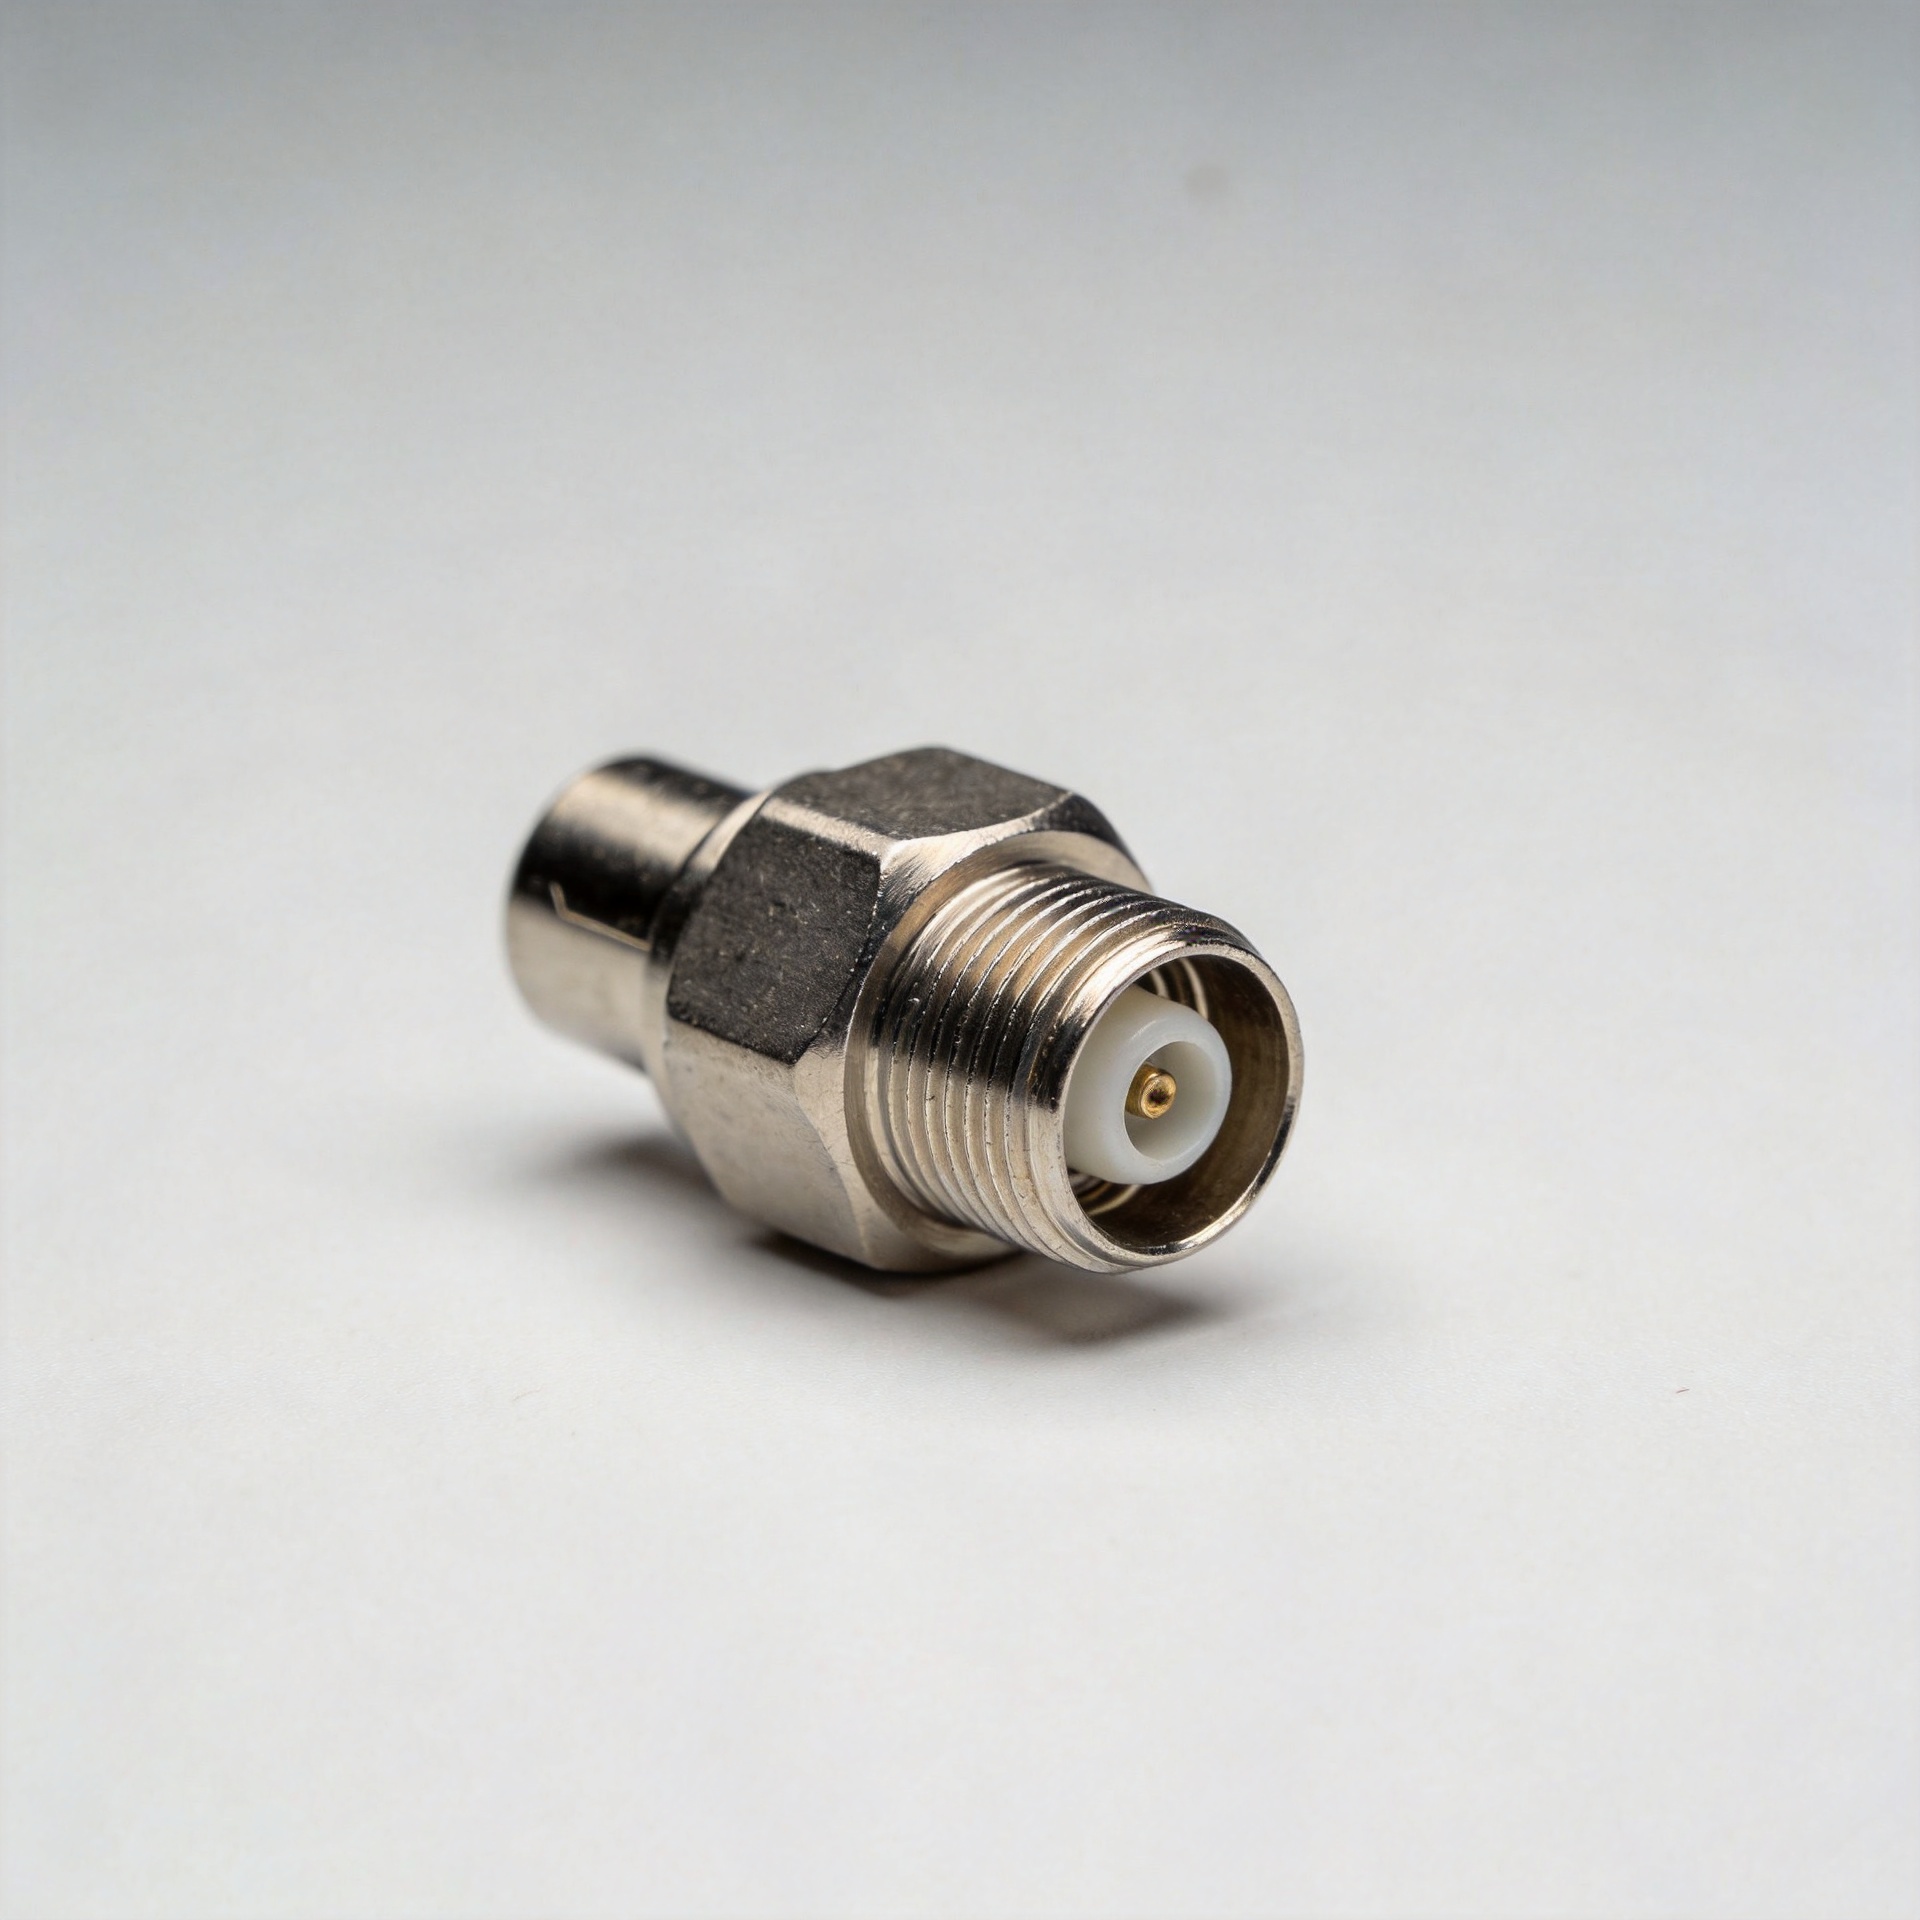
For an OEM buyer, an n type connector is not simply a threaded RF part on a purchase order. It is a mechanical interface, an electrical transition, and a traceability point in the same system. A quality plan for an n type connector must therefore prove more than appearance. It should show that the supplied configuration matches the approved design, that production stays controlled, and that the released lot can be identified if a question arises later.
This matters most when the same n type connector is used across repeated builds, outdoor assemblies, test fixtures, or antenna-feed hardware. Small variations in material, interface dimensions, plating, assembly practice, or documentation can create an avoidable investigation for the OEM. The practical goal is straightforward: define acceptance criteria before production, then collect evidence at the points where a defect could enter the process.
Start with an approved specification, not a generic name
The label n type connector alone is incomplete. A supplier should convert the OEM drawing or RFQ into a controlled specification covering gender, impedance, termination style, cable compatibility where relevant, mounting arrangement, material and plating requirements, applicable frequency range, environmental expectations, packaging, and required records. For context, IEC 61169-16 covers type N RF coaxial connectors and includes 50-ohm versions; the exact product rating and applicable revision still need confirmation for the intended assembly.
That review is where a capable supplier catches mismatches before metal is cut or components are issued. An n type rf connector for a bulkhead installation, for example, may need different dimensional checks from an n type rf connector used in a cable assembly. The supplier should record open points, obtain disposition, and lock the approved configuration. It is far less expensive to clarify a coupling interface or cable preparation detail at this stage than after a production lot is complete.
Control incoming materials and approved sources
Strict quality control begins before assembly. For every n type connector, incoming inspection should verify that the received component or raw material corresponds to the approved part number and revision. Depending on the requirement, the inspection plan may include visual condition, critical dimensions, plating appearance, thread engagement, dielectric condition, certificates, and supplier-lot identification.
A useful control is an approved-source list combined with lot segregation. If the contact, body, insulator, or cable component changes, the change should not disappear into routine purchasing. The supplier should evaluate the impact, notify the OEM when the agreement requires it, and preserve the old and new lot identity. This discipline helps prevent a seemingly equivalent n type connector from behaving differently across production runs.
Use first-article approval to validate the process
Before a production release, the supplier should build a first article under normal process conditions. The first article is not a showroom sample; it is evidence that the planned tooling, work instructions, operators, and inspection methods can produce the requested n type connector. The record should link measurements and test results to the exact configuration being approved.
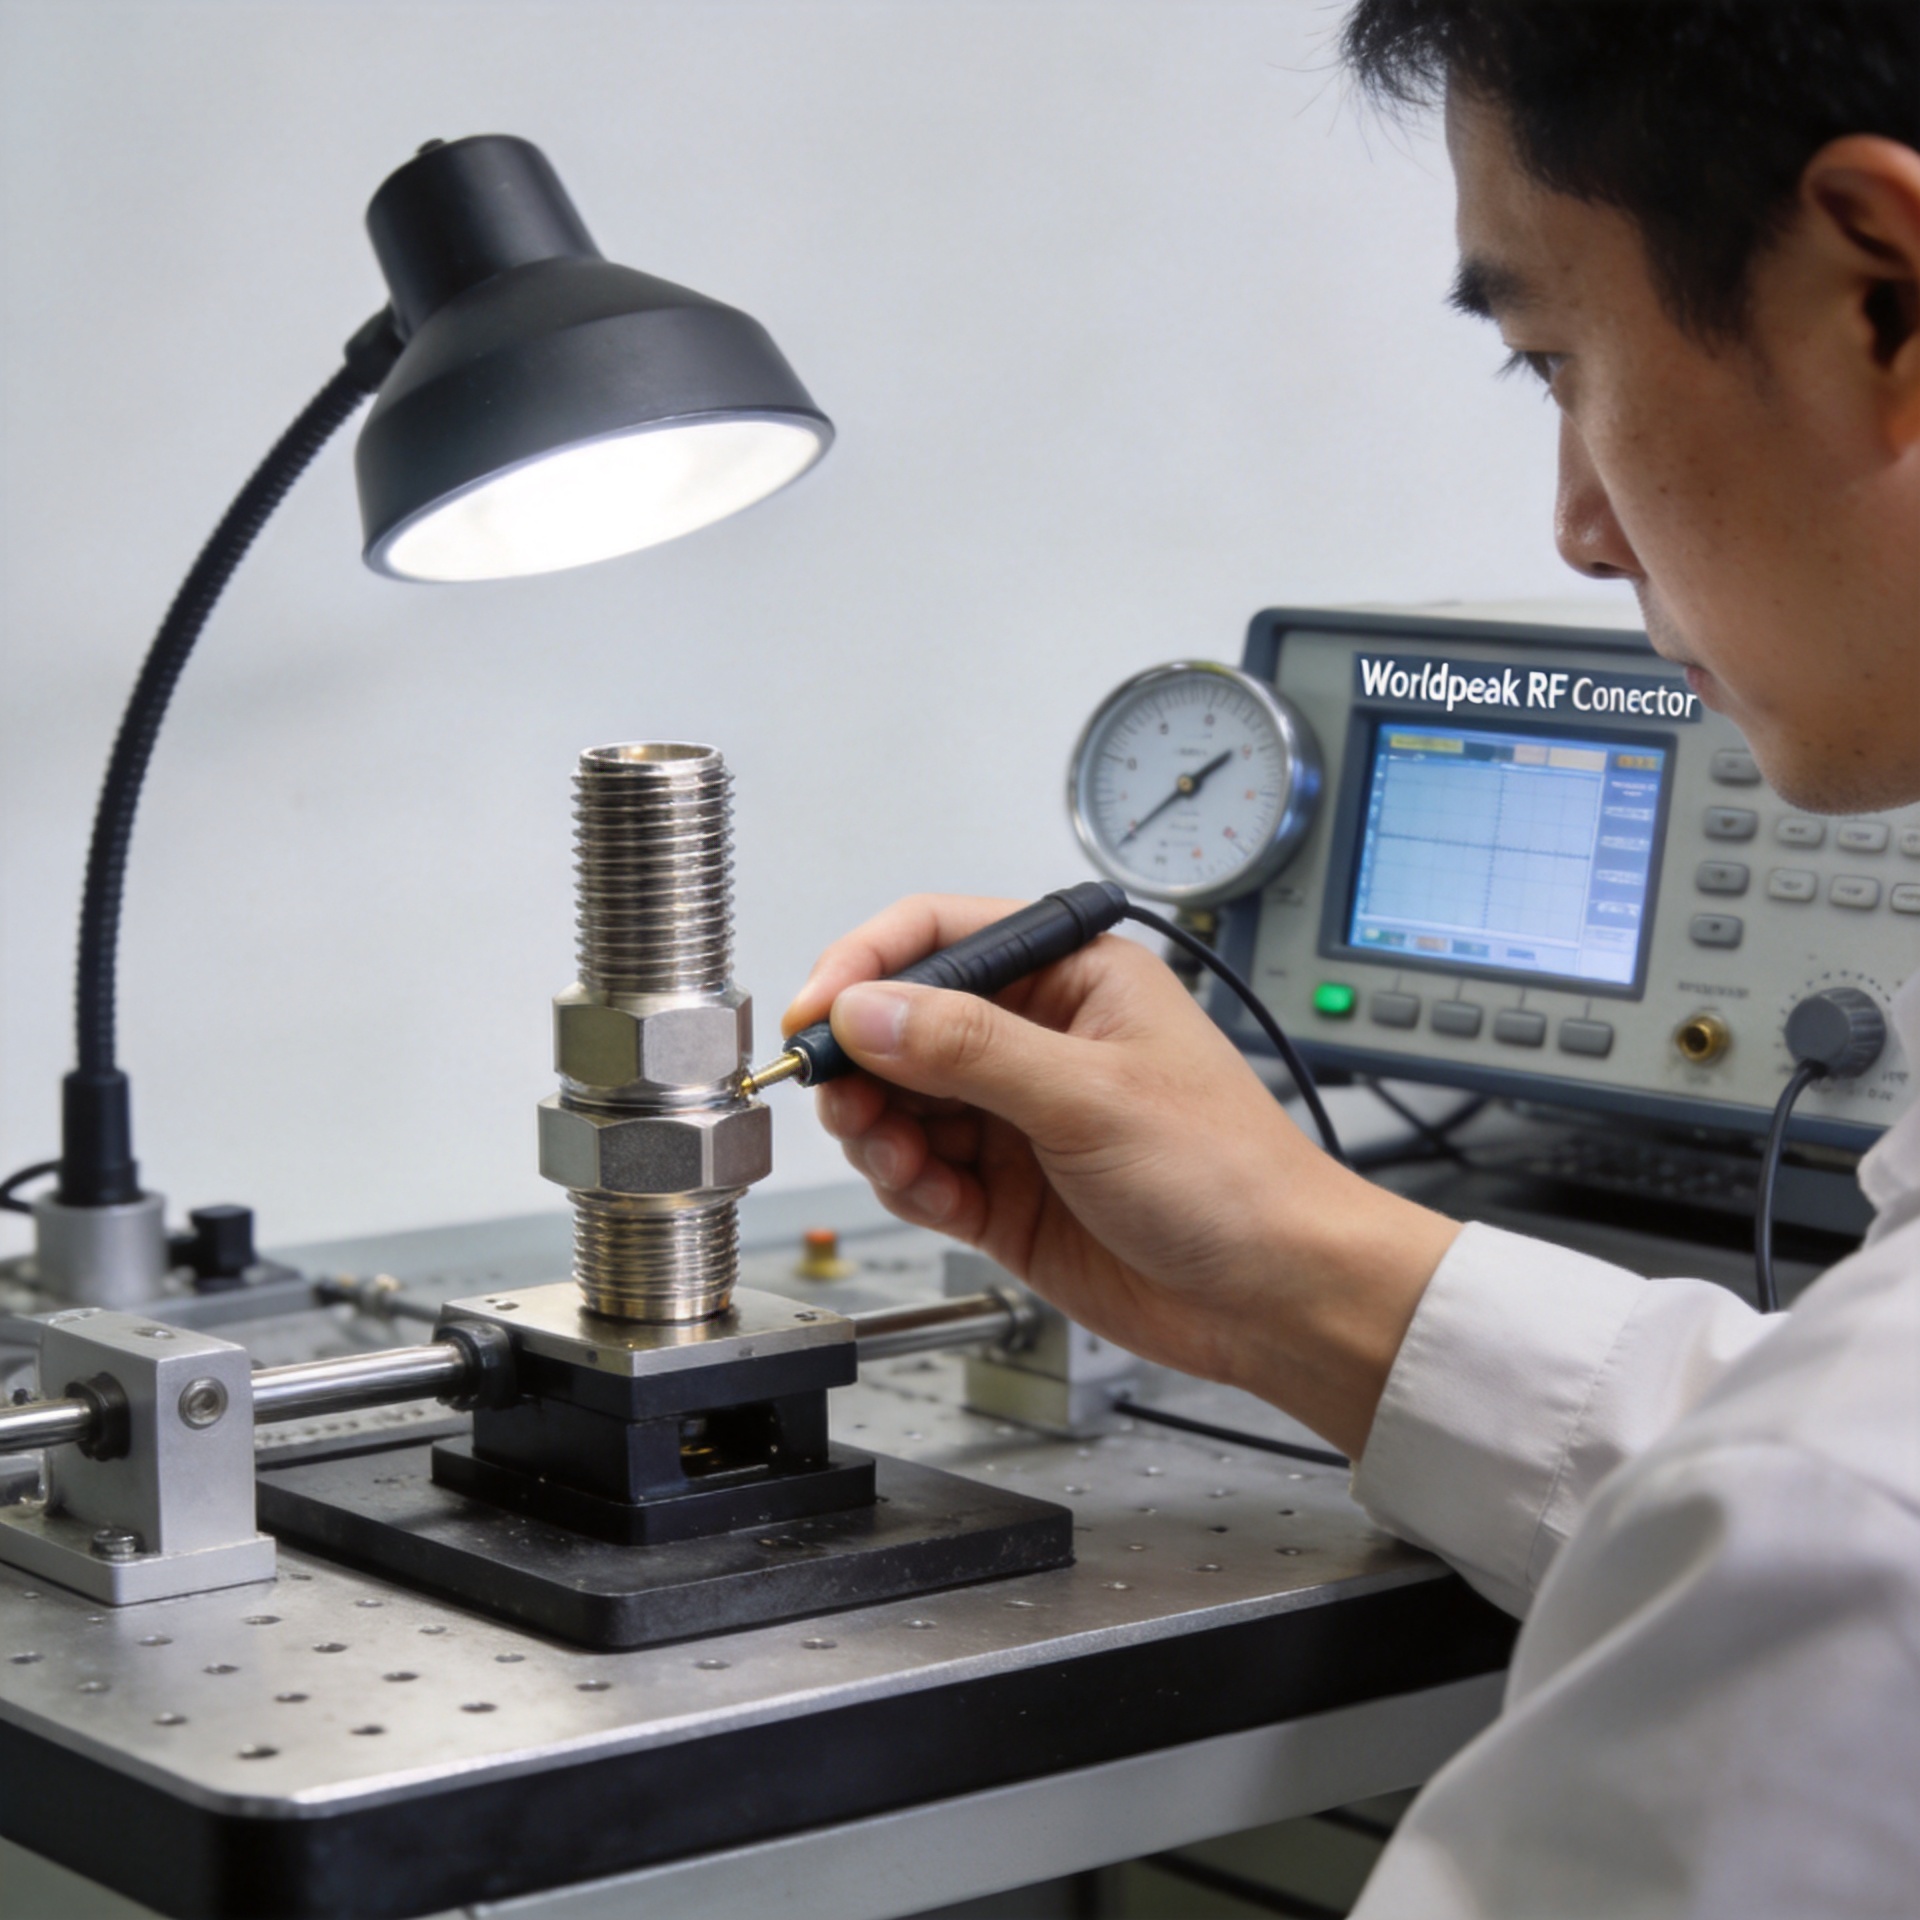
For an OEM n type connector program, first-article evidence commonly includes interface dimensions, mating checks, visual workmanship, and the agreed electrical checks. If the part is part of a terminated cable assembly, pull resistance, continuity, insertion loss, return loss, or VSWR checks may also be appropriate. The scope should follow the agreed specification rather than a generic checklist. A supplier that documents why a check applies is easier to qualify than one that merely says every unit is inspected.
Make assembly controls repeatable
Once the first article is accepted, work instructions translate the approval into repeatable action. For an n type connector, instructions should identify the correct components, fixtures, stripping or crimping dimensions when applicable, torque or tightening controls, visual checkpoints, and handling rules. Calibrated tools matter because a connection that looks acceptable can still have mechanical or RF consequences if the process is inconsistent.
In-process inspection is especially valuable at irreversible steps. A technician can confirm component identity and preparation before termination, while a supervisor or quality inspector can verify critical characteristics before the assembly moves to final test. This is where an n type rf connector program becomes controlled manufacturing rather than end-of-line sorting. Rework should be recorded, assessed, and limited by clear acceptance rules; repeated rework is a signal to review the underlying process.
Verify electrical and mechanical performance before release
Final inspection should reconcile the finished n type connector against the purchase requirement and the first-article baseline. A release record can include a visual inspection, dimensional or gauge checks, mating verification, labeling review, and the agreed electrical tests. For cable assemblies, Worldpeak's shared capability profile states that pre-shipment insertion-loss and VSWR sweep measurement can be performed and test data included in shipment documentation. Buyers should define the sampling level, frequency range, limits, and record format in their inspection plan.
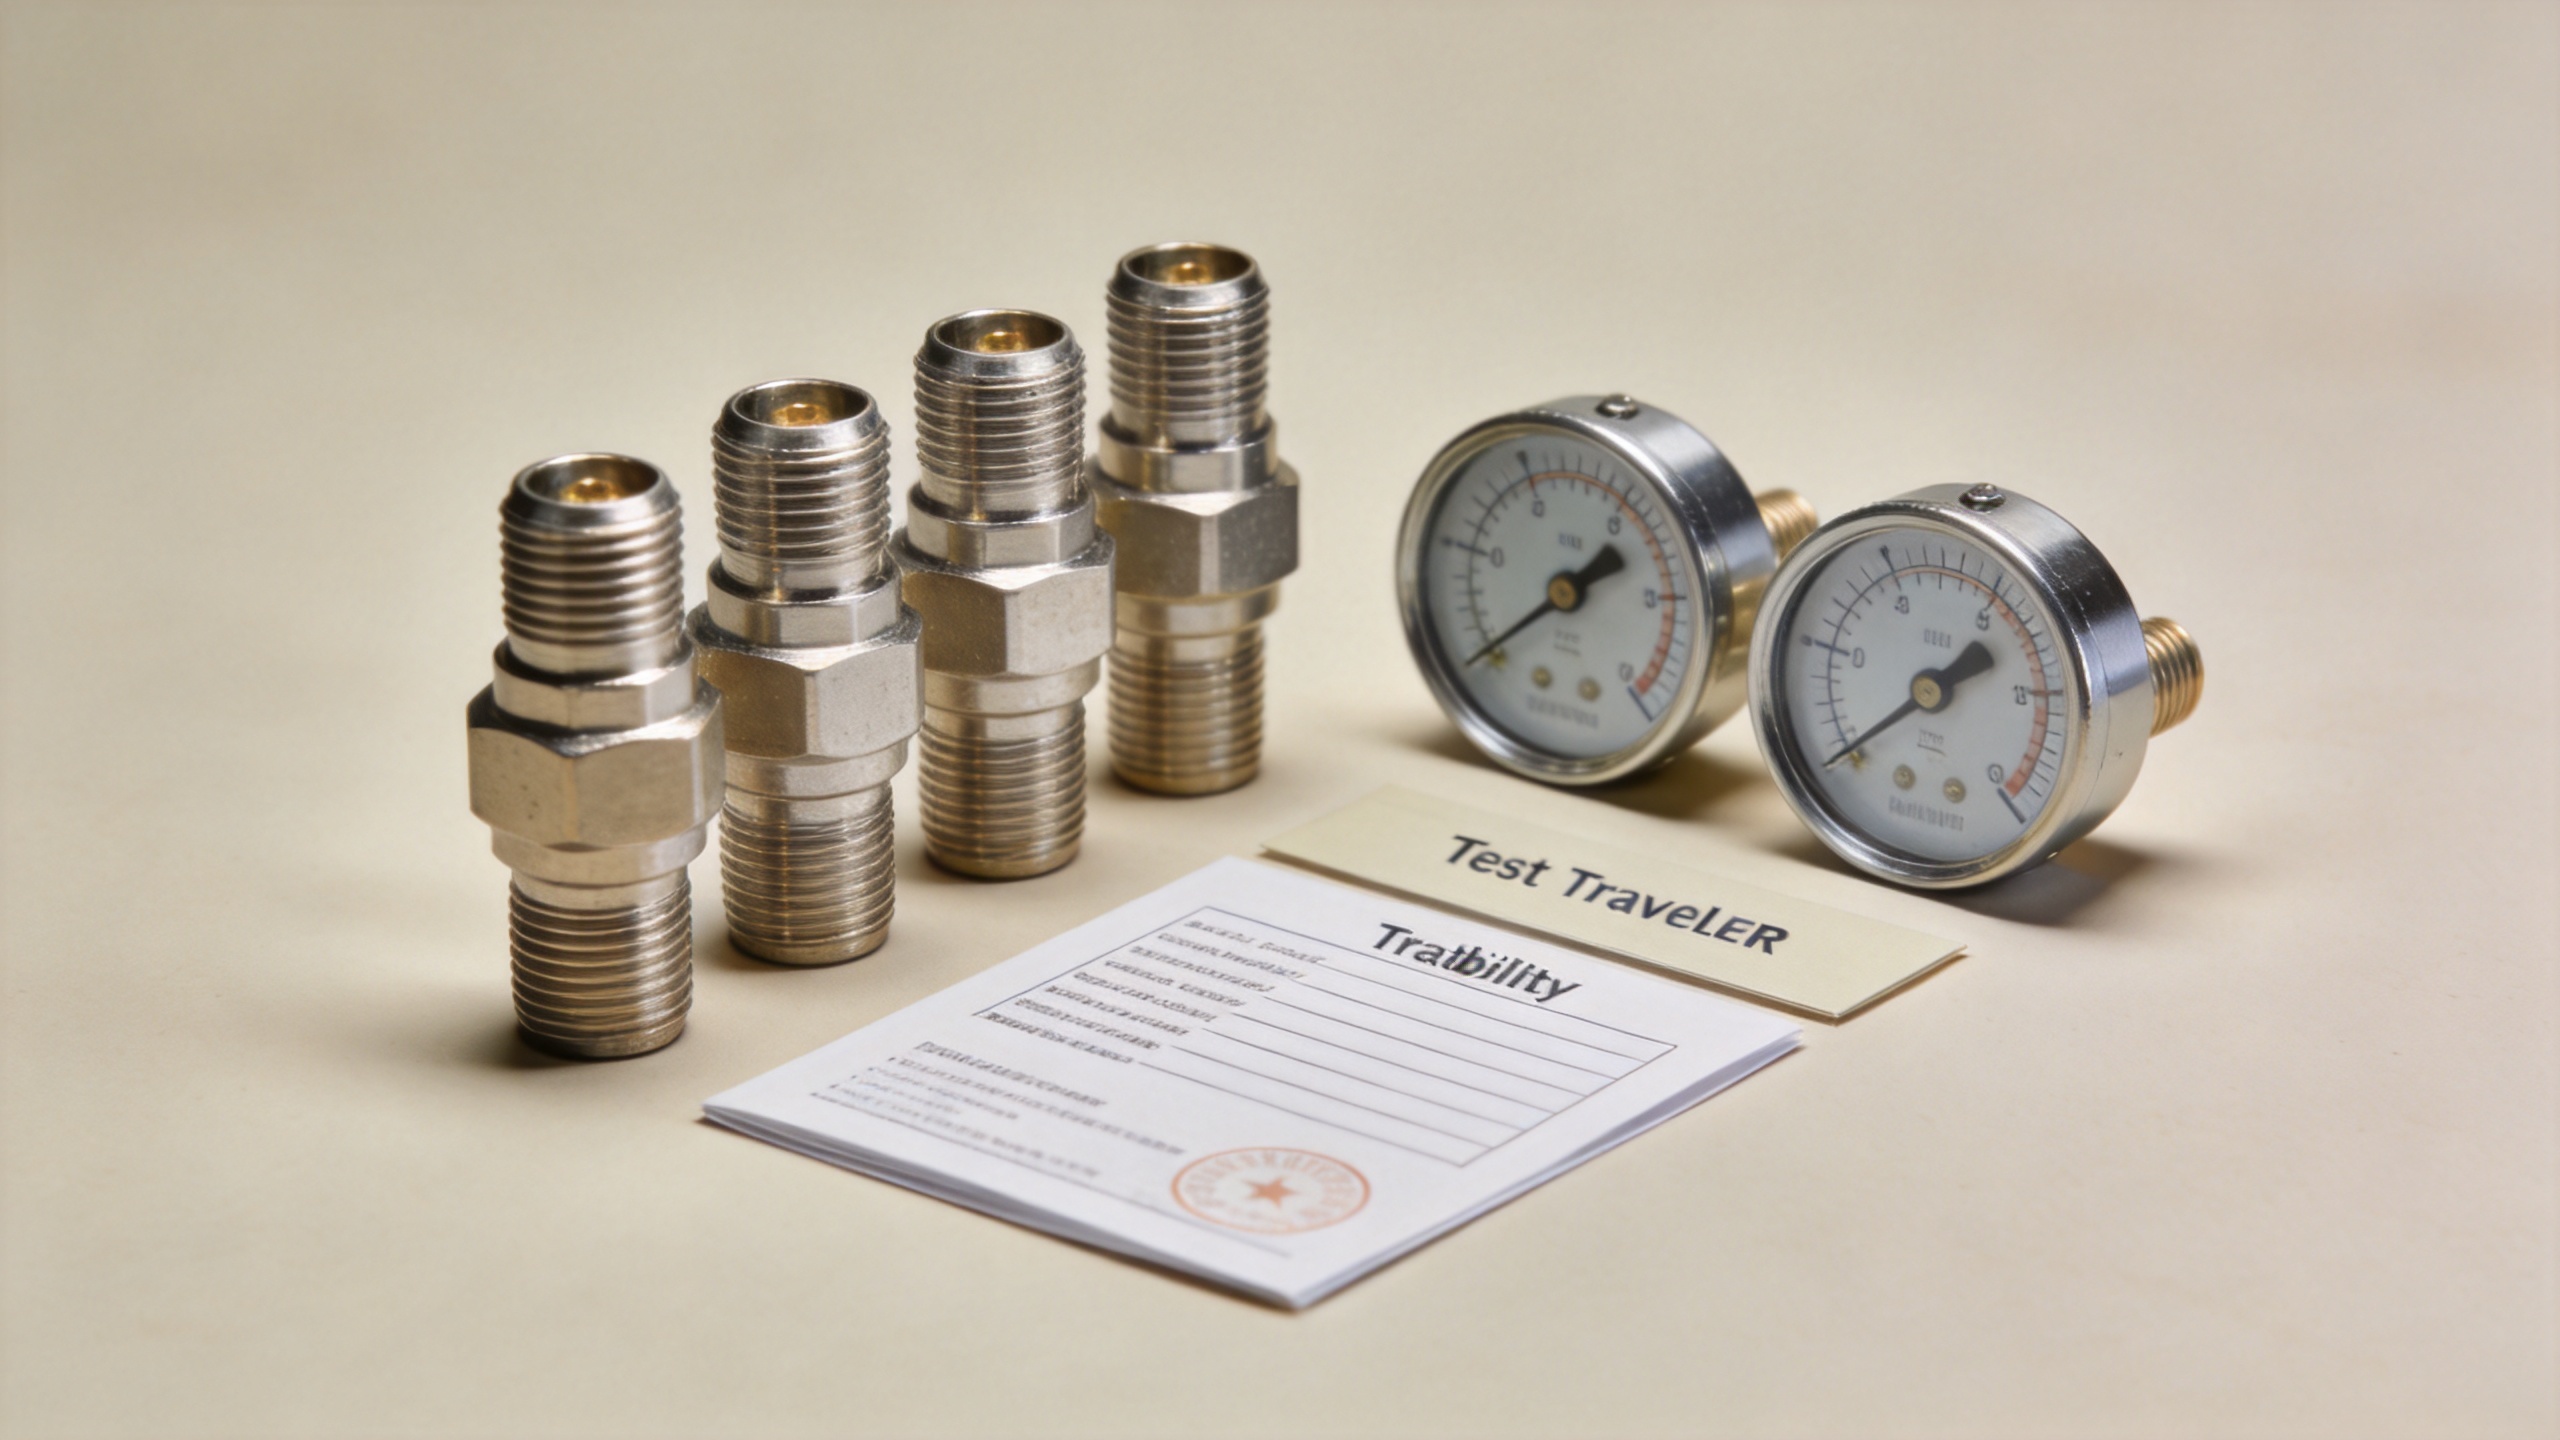
Do not treat a pass/fail label as the whole story. An OEM should be able to ask which lot was tested, which equipment was used, whether calibration was current, and what configuration was tested. A traceable n type connector release packet makes incoming inspection faster because the buyer can compare documents with the approved requirements instead of reconstructing the supplier process from scratch.
Build traceability into labels, packaging, and change control
Traceability closes the loop. Each shipment of n type connector components should be linked to a part number, revision, manufacturing or inspection lot, quantity, date, and associated report where required. Packaging must protect the mating interface and preserve lot separation. Clear labels also reduce mix-ups when similar n type connector variants arrive together for production.
Change control is equally important. A supplier should not substitute a material, plating source, insulator, tooling method, or test sequence without a documented review. The OEM may permit some changes, require notification for others, or require a new first article. That boundary is not bureaucracy; it protects RF performance and keeps the qualified product aligned with the product that is actually shipped.
An OEM-facing quality checklist
- Is the n type connector specification complete and revision-controlled?
- Are incoming components and production lots identified and segregated?
- Does the first article represent normal production methods?
- Are irreversible assembly steps governed by documented instructions and calibrated tooling?
- Do final records show the agreed electrical and mechanical verification for the n type connector?
- Can the supplier provide a lot-level release record and manage changes before shipment?
A strict program does not promise that every application has identical tests. It creates a visible chain from requirement to verification. When OEM buyers evaluate an n type rf connector supplier, that chain—approved specification, controlled materials, first article, in-process discipline, final evidence, and traceability—is the clearest indicator that quality control is being implemented rather than simply claimed.